The choice depends less on the method’s name than on the decision needed. Designing a strategy for a new critical system, checking an established plan and removing a few duplicate tasks require different depths. Define failure consequences, existing-plan quality and available expertise first. A poorly scoped shortcut may leave risks unexamined; an exhaustive analysis without implementation resources may remain on paper.
What an RCM process means
Reliability-centred maintenance, or RCM, starts with an asset’s required functions in its operating context. It examines functional failures, failure modes, effects and consequences before selecting tasks or other actions. SAE JA1011 provides criteria for evaluating RCM processes. RCM is not simply a criticality table or a list of manufacturer inspections.
“Reverse RCM”: define the actual scope
“Reverse RCM” is used for some approaches that start from existing tasks and work back to the failure modes they are intended to address. Do not infer an ISO or SAE standardized method under that name. Vizory uses the term in its Rio Tinto Fer & Titane strategy-review case. Ask explicitly how missing failure modes are identified: reviewing only existing tasks cannot uncover every risk.
| Approach | Starting point | Limitation to manage |
|---|---|---|
| RCM | Functions, context and consequences; a strategy to build or reassess comprehensively. | Requires expertise, operations involvement and implementation time. |
| Review described as reverse RCM | Existing tasks, followed by justification against target failures. | Explicitly seek missing modes and clarify the criteria used. |
| Preventive optimization | Existing plan, results, duplicates, intervals and instruction quality. | A focused review does not necessarily constitute full RCM. |
Two contrasting situations
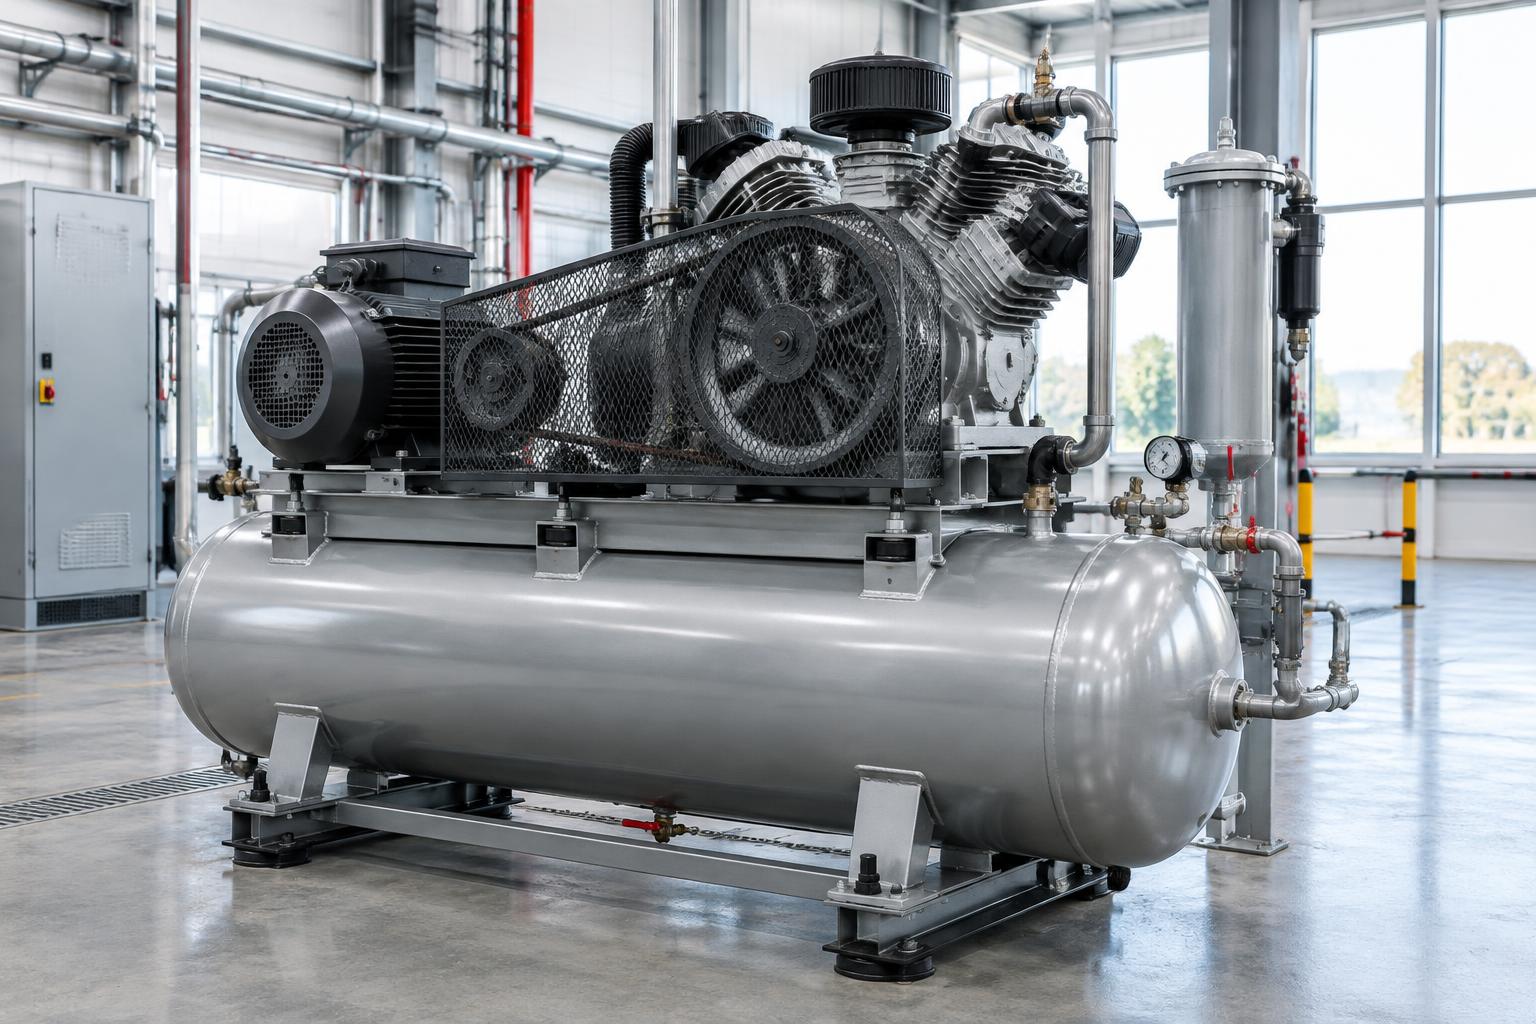
Fictional scenario A: a new compressor performs a critical function without redundancy. Little history exists. Analysis based on functions, design, consequences and technical experience is more defensible than simply cutting tasks. Involve the manufacturer and operations. An absence of failure data does not justify an absence of strategy.
Fictional scenario B: a conveyor family has old plans, usable histories and many identical tasks. A focused review can begin with duplicates and observed modes, then check uncovered modes. Speed comes from scope and available information, not relaxed safety requirements.
Questions to ask before starting
- Which assets and functions are included? What is explicitly out of scope?
- Who validates consequences, legal requirements and manufacturer recommendations?
- How are failure modes missing from history and the plan identified?
- Does the deliverable include executable instructions, task rationale and an implementation plan?
- Which measures will verify that the revised strategy remains effective?